Special alloy manufacturer & exporter · Shanghai, China

demi@nickel-alloy.com  |  +86 15618279078  |  WhatsApp

Technical knowledge

Flange facing types: raised face, flat face, ring joint and tongue and groove

How raised face, flat face, ring type joint, tongue and groove and male and female facings work, which gasket each needs, and how to choose the right facing for pressure, temperature and fluid.
Published Last updated 8 minute readCategory: Technical knowledge
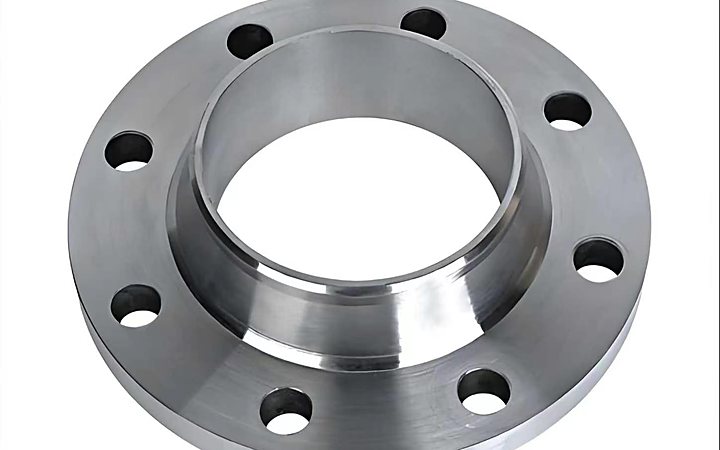
Weld neck flange showing machined raised face and serrated finish
Machined raised face with serrated finish ready for a spiral wound gasket.

The main facing types and what they do

Common facings and their application
FacingHow it sealsTypical gasketWhere it is used
Raised face, RFConcentrates bolt load on a narrow ringSpiral wound to ASME B16.20Default for process piping
Flat face, FFLoad spread across the full surfaceFull face soft gasketCast iron, brittle and dissimilar mates
Ring type joint, RTJMetal ring deforms into a grooveR or RX or BX ringHigh pressure and high temperature
Tongue and groove, T and GGasket confined on all sidesConfined ring or sheetHigher integrity, limited movement
Male and female, M and FGasket confined by a recessConfined ringWhere alignment is controlled

Surface finish: the detail that decides most leaks

The raised face finish is specified as a concentric or spiral serrated groove, typically in the range of 3.2 to 6.3 micrometres average roughness. A face that is too smooth allows the gasket to creep or blow out; a face that is too rough will not seal with a metallic or semi metallic gasket. Always state the finish on the order and protect the face during handling, storage and installation.

Rules for ring type joints

  • The groove must be harder than the ring. The ring is the sacrificial component and must deform first.
  • State the groove hardness. Agree a hardness window appropriate to the flange material and the ring.
  • Do not reuse rings. A ring that has been compressed will not seal again.
  • Protect the groove. Any dent or corrosion in the groove is a leak path.

How to choose in practice

Start from the piping class and the mating equipment. Use raised face with a spiral wound gasket for most services. Move to ring type joint for high pressure classes, for high temperature, or where the piping class already specifies it. Use flat face only where the mating flange would be damaged by the concentrated load of a raised face, such as cast iron or certain non metallic components.

Questions about this topic

Can I machine a raised face into a ring type joint groove later?
Yes, if the flange has sufficient remaining thickness and the modification is approved by the piping engineer. It changes the rating and the gasket arrangement, so it must be assessed rather than assumed.
What surface finish should I specify?
A concentric or spiral serrated finish in the range typically quoted for raised face flanges, with the roughness value stated on the order. Confirm the value against the gasket manufacturer recommendation.
Why do ring type joint grooves need a hardness limit?
Because the ring must deform to create the seal. If the groove is softer than the ring, the groove deforms instead and the joint leaks, and the flange is then damaged rather than the replaceable ring.

Questions about our products

What products does Hangbo Alloy supply?
Four product families, all available in nickel-based alloys, titanium, duplex and special stainless steel: flanges, butt weld pipe fittings, elbows, and seamless tube and pipe. Flanges cover weld neck, long weld neck, slip-on, blind, socket weld, threaded and lap joint patterns. Fittings and elbows cover concentric and eccentric reducers, equal and reducing tees, caps, stub ends, and 45°, 90° and 180° returns in both long and short radius, plus 3D and 5D bends for piggable lines. Seamless tube and pipe is supplied cold drawn or hot finished from 6 mm to 630 mm outside diameter.
Which alloy grades are available for these products?
More than 90 grades are published in our grade library. The most requested are Inconel 625, 718, 600 and X-750, Hastelloy C-276, C-22 and B-2, Monel 400 and K-500, Incoloy 800H, 825 and 925, duplex 2205 and super duplex 2507, 316L, 904L and 254SMO stainless steel, and titanium Grade 2 and Grade 5. Nickel-based grades can also be supplied with VIM plus ESR double melting where cleanliness or fatigue life is critical.
What sizes, wall thicknesses and pressure classes can you supply?
Flanges run from NPS ½ to NPS 24 to ASME B16.5 and from NPS 26 to NPS 60 to ASME B16.47 Series A or B, in pressure classes 150 through 2500. Butt weld fittings and elbows run from NPS ½ to NPS 48 (DN 15 to DN 1200) in wall thickness Schedule 5S through XXS. Seamless tube and pipe covers 6 mm to 630 mm outside diameter, in random lengths of about 5 to 7 metres or fixed lengths up to 12 metres. Non-standard and intermediate sizes are quoted on request.
Which material and dimensional standards do you work to?
Forged flanges to ASTM B564, B381 and A182 with dimensions to ASME B16.5 and ASME B16.47. Butt weld fittings and elbows to ASTM B366 and A403 with dimensions to ASME B16.9 and MSS SP-43. Seamless tube and pipe to ASTM B444, B423, B622, B163, B167, B861, A312, A213 and A790. Marking follows MSS SP-25 and the applicable product standard. If your project is governed by EN, DIN, JIS or a company specification, send the document and we will confirm equivalence before quoting.
Is there a minimum order quantity?
There is no minimum for standard sizes and grades held in stock, and prototypes, spares and small trial batches are accepted. Made-to-order melts and special forgings carry a minimum weight that depends on the alloy and the route, typically from about 500 kg for special grades.
What inspection and certification is issued with the goods?
Every shipment carries an EN 10204 3.1 mill test certificate quoting the actual chemical and mechanical results for the specific heat lot, together with dimensional records and heat treatment data where applicable. Testing is carried out in house by optical emission spectrometry, tensile, impact and hardness testing, plus ultrasonic and eddy current examination, with hydrostatic pressure and intergranular corrosion testing to ASTM G28 or A262 Practice E where the specification requires it. Third party inspection by SGS or another recognised agency can be arranged, and their report is issued alongside the shipment.
What are typical lead times?
Standard stock items ship within days. Common production grades such as Inconel 625 or duplex 2205 are typically a few weeks. Special chemistries, larger forgings and items that require third party inspection take longer and are quoted individually against the requirement.
How are the products packed for export?
Flanges and fittings receive a rust preventive coating, are individually wrapped and are packed in plywood cases secured with steel banding. Tube ends are capped and bundles are strapped. Packing lists quote heat numbers so every case can be cross-checked against the mill certificate on arrival. We quote EXW, FOB, CFR, CIF and DAP, and mixed-alloy orders can be consolidated into one shipment with a single documentation package.
How do I request a quotation or a sample?
Send the grade or UNS number, the dimensions including schedule or wall thickness, the governing material and dimensional standards, quantity, any heat treatment or NDT scope and the certificate type you need; a drawing is ideal for special flanges and fittings. Email demi@nickel-alloy.com or message us on WhatsApp +86 15618279078 and we normally issue a formal quotation within 24 hours on working days. Samples and previous test reports can be arranged before the first order.

Written by Hangbo Alloy Technical Team

Metallurgy & materials engineering. Reviewed against the latest ASTM, ASME and AMS specifications held on file at Hangbo Alloy. Last updated 2026-09-18.

Questions on this specification? Email demi@nickel-alloy.com or WhatsApp +86 15618279078.

Continue reading

Ready to specify your alloy?

Send us your drawing, material specification and quantity. You receive a formal quotation within 24 hours, including melting route, heat treatment, testing scope and certificate format.